PTFE Gland Packing Manufacturer Guide to Choosing Dependable Sealing Solutions
2026-10-31
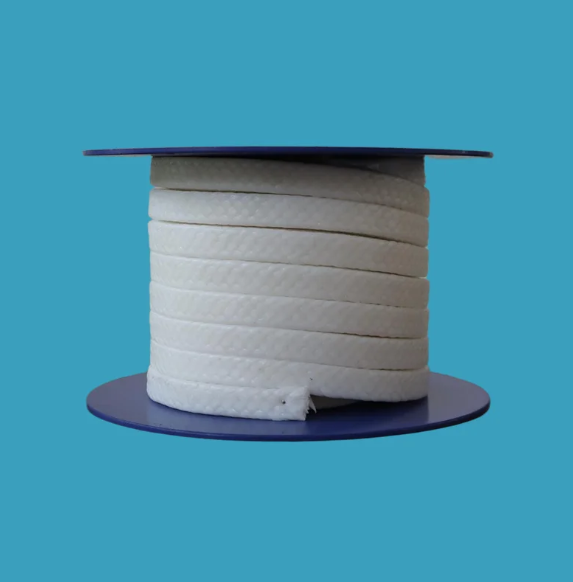
Most PTFE gland packing fails not because of the material, but because someone chose the wrong manufacturer. You can have the finest PTFE yarn and still end up with leaks, shredding, or premature wear if the braiding density, lubricant, and finishing aren't controlled with precision. This guide is built for maintenance and procurement professionals who are tired of guessing. It walks through the practical factors that separate a truly dependable PTFE gland packing manufacturer from the rest—without the marketing fluff. If you're evaluating suppliers, you'll find clear, actionable criteria here. And when you're ready to see those criteria in action, TAIFNO has the track record to back it up.
What Separates Dependable PTFE Packing From the Rest
Most PTFE packing looks nearly identical on a shelf, but the differences show up quickly under load. Dependable versions start with high-purity resin and controlled sintering, not regrind blends that leave hard spots and uneven density. That baseline matters because it determines how the packing beds in, how it handles temperature swings, and whether it holds its shape instead of extruding into the stuffing box clearance.
Another separator is filler choice and dispersion. Graphite, carbon, and glass are common, but cheap formulations can clump or settle, creating uneven hardness around the ring. In practice that means one side of the packing wears fine while the other overheats or scores the shaft. Reliable products keep the filler evenly distributed, so friction stays predictable from the first adjustment to the last repack.
The final difference is how the material behaves over time. Dependable PTFE packing doesn't demand constant gland chasing; it settles once, keeps a light film on the shaft, and tolerates minor misalignment without turning brittle. If a packing runs dry for a short period or sees a temperature spike during startup, it shouldn't crack or lose its lubricity permanently. That kind of performance comes from process control and tight tolerances, not just the resin name on the box.
Reading Your Equipment’s Needs Before You Pick a Packing Style
Every piece of equipment brings its own set of demands to the packing table. A rack-mounted server shrugs off a few bumps but hates moisture and dust, while a handheld barcode scanner can survive a drop yet suffers when its trigger gets pressed during transit. You can’t just grab the same foam and box for both. Start by looking at what the device actually fears: vibration, compression, static discharge, temperature swings, or maybe just its own weight shifting inside the carton. That list, not some generic checklist, should drive the packing choice.
Consider a laser alignment tool next to a ruggedized field laptop. The tool might weigh less than two kilos but its optics demand a rigid shell with custom-cut foam that holds every axis still. The laptop, on the other hand, can ride in a softer padded sleeve as long as the corners get extra protection and the screen faces away from pressure points. Reading the equipment means noticing those small vulnerabilities—an exposed connector, a glass display, a calibration screw that drifts if jarred—and then asking which packing style actually addresses them.
Once you’ve mapped the equipment’s weak spots, the packing style almost selects itself. Heavy items need structural support, not just cushioning. Devices with vents or filters call for breathable wraps or desiccant packs instead of fully sealed bags. And anything with a battery or circuit board deserves anti-static material touching it directly. The trick is to stop thinking about packing as a one-style-fits-all routine and treat it as a response to what the equipment is telling you before the box even closes.
The Installation Habits That Quietly Destroy Gland Life
Most technicians never connect a premature gland failure to the way the unit was originally installed. The damage happens slowly, often hidden behind normal operating noise. A slightly over-tightened follower, a barely misaligned shaft, or a handful of abrasive particles left on the sealing surface all work quietly against the gland. By the time leakage becomes obvious, the root cause is already weeks old.
One of the most damaging habits is using a standard wrench to force the gland follower down without checking torque values. This crushes the packing or seal ring far beyond its design limit, generating extra friction and heat that break down the material long before its rated service life. Another silent killer is skipping the cleaning step. Even fine dust or metal shavings left on the shaft or inside the stuffing box act like sandpaper, scoring the gland neck and creating leak paths that widen over time. Using whatever grease is nearby can also be harmful. Many generic lubricants cause certain seal materials to swell or soften, which changes the sealing geometry and accelerates wear.
Changing these habits doesn't require new equipment or advanced training. A torque wrench, a clean rag, and the manufacturer's recommended lubricant are usually enough. Before assembly, wipe the shaft and gland bore until they are completely clean, check runout with a dial indicator, and tighten the follower gradually in a star pattern. These small adjustments remove the hidden stresses that quietly destroy gland life, and they cost far less than replacing a failed gland in the middle of a shift.
Balancing Friction, Heat, and Leakage Without Over-Tightening
A common mistake is treating torque as the only variable that matters. Threaded fasteners rely on a subtle interplay between clamping force and the energy lost to friction under the head and in the threads. When you chase a higher torque value simply to stop a leak, you often end up adding more heat than sealing capability. The joint distorts microscopically, the gasket loses its ability to rebound, and the fastener itself begins to creep. Instead of forcing the connection tighter, think about managing the friction zones first—clean threads, proper lubrication, and flat, parallel mating surfaces can deliver a consistent clamp load at a lower applied torque, leaving more margin before yield.
Heat complicates things quickly. A joint that seals perfectly at room temperature can open up as components expand at different rates. Over-tightening makes this worse because it leaves no room for thermal movement; the gasket gets squeezed beyond its elastic range, then cannot recover when the assembly cools. Rather than preloading everything to the maximum, select a target clamp load that keeps the gasket in its working compression range across the entire temperature swing. Use torque plus angle or direct tension monitoring where possible, because turning the bolt a specific number of degrees tells you more about actual stretch than a torque wrench ever will.
Leakage is often a symptom of uneven load, not insufficient total load. If the flange faces are not parallel or the bolt pattern is tightened in the wrong sequence, a few fasteners carry most of the load while others are barely snug. No amount of extra torque on the tight ones will fix a gap on the opposite side—it just warps the assembly further. Work through the pattern in small increments, using multiple passes, and verify the joint with a feeler gauge or leak test before adding more torque. The best seal comes from a balanced, evenly distributed clamp load that stays stable under operating conditions, not from the highest number on the wrench.
Chemical Exposure Charts Are Only Half the Story
Chemical exposure charts tend to get treated like quick-reference bibles, but they only tell you a fraction of what is actually happening. A single number might look authoritative, yet it often hides the conditions under which that limit was measured. Was it an average over a full shift, a ceiling value, or something in between? Without knowing the time frame, frequency, and route of exposure, that number can mislead as much as it informs. Real-world exposure rarely matches the neat assumptions baked into a chart.
Even when a chart is accurate for its intended context, it cannot account for who is being exposed. Two people can have wildly different responses to the same concentration. Age, liver function, pregnancy, existing respiratory conditions, and even genetic variations in detoxification enzymes all shift the threshold for harm. A chart built around a healthy adult male worker may offer little protection to a pregnant woman or a teenager with asthma. Treating everyone as statistically identical is a dangerous oversimplification.
Perhaps the biggest blind spot is that most charts focus on one chemical at a time. In practice, people breathe, touch, and ingest mixtures. Solvents, metals, and dusts often appear together, and their combined effects can be additive or synergistic, meaning the whole is worse than the sum of its parts. A chart cannot tell you how benzene and toluene interact in your bloodstream, or how chronic low-level exposure stacks up over years. If you stop at the chart, you miss the larger story of how chemicals actually behave in real bodies and real workplaces.
When Custom PTFE Blends Pay Off in Real-World Pumps
Real-world pumps rarely see clean, predictable fluids. Standard PTFE handles many jobs, but custom blends pay off when the fluid pushes pure PTFE past its comfort zone—hot acids carrying abrasive fines, solvents that cause creep, or dry-running conditions that spike local temperatures. Fillers like carbon fiber, glass, or specialty polymers are not added for marketing reasons; they change how the material behaves under actual pump loads.
Consider a chemical transfer pump moving concentrated sulfuric acid at 120 °C with catalyst particles in suspension. Pure PTFE seats and seals may extrude or erode within a few weeks. A custom PTFE blend with carbon fiber and graphite reduces wear and improves heat transfer enough to stretch service life several times longer. In food-grade diaphragm pumps, a mineral-filled PTFE blend can keep friction low while surviving clean-in-place cycles that would attack other materials.
The real payoff shows up as fewer unplanned shutdowns, less leakage, and fewer rebuilds. Most engineers arrive at a custom blend after a failure investigation, not from a catalog. Once the blend matches the actual fluid, temperature, and mechanical load, a simple wear part turns into a reliability upgrade.
FAQ
PTFE offers very low friction, broad chemical resistance, and can handle temperatures from -100°C to +260°C. When manufactured with proper density and break-in behavior, it seats quickly without scoring shafts or stems. That combination keeps leakage under control without demanding constant retightening.
Start with the chemical compatibility chart, but also think about pH swings, abrasive particles, and whether the fluid is a solvent or oxidizer. Pure PTFE works well for aggressive acids and caustics, while filled grades such as graphite or glass-loaded are better where heat dissipation or creep resistance matters.
Look for clear material traceability, consistent density from batch to batch, and the willingness to share friction and compression data. A dependable manufacturer will also ask about your shaft speed, runout, and stuffing box depth instead of just pushing a generic product.
Yes, but only if the packing is properly cross-braided and the gland load is kept modest. High speed generates more frictional heat; unlubricated PTFE can transfer to the shaft if overloaded. So choose a grade designed for higher speed and monitor stuffing box temperature during initial run-in.
PTFE consolidates during the first hours of operation. If you tighten it to zero leakage right away, it will overheat and burnish. Instead, start with a slight leak, let the packing bed in, then tighten gradually over several hours until leakage drops to an acceptable level.
Not universally. Pure PTFE is cleaner and non-contaminating, which suits food or pharmaceutical duties. Graphite-filled grades shed heat faster and resist extrusion at high pressure. The choice depends on whether you need purity or mechanical resilience at the operating point.
Cutting rings straight instead of on a mandrel causes gaps and uneven compression. Also, using a dull blade frays the edges. Cut each ring on a mandrel of the shaft diameter, with clean square or skive joints, and check that the ends meet without overlap.
Watch for signs like persistent shaft scoring, excessive heat at the gland, rapid volume loss, or extrusion into the clearance gap. If you're constantly retightening to control leakage, the packing likely lacks the right filler, density, or cross-section for the service conditions.
Conclusion
Dependable PTFE gland packing is rarely about the resin alone. The real difference shows up in how the yarns are treated, how tightly the braid is controlled, and whether the supplier digs into your pump's speed, runout, pH swings, and any abrasive particles in the fluid. Two pumps that look identical on a nameplate can demand entirely different packing because one has a slight shaft misalignment and the other runs with frequent stops and starts. That is why reading your equipment's needs before picking a style matters far more than chasing a higher PTFE percentage. A packing that holds up in clean water may fail quickly in a stream that swings from acidic to alkaline or carries fine solids through the stuffing box.
Poor installation destroys gland life faster than most chemical attacks. Rings cut too short, opened with a dull pick, or jammed into a worn stuffing box create uneven loading before the pump reaches full speed. The quiet skill is balancing friction, heat, and leakage without leaning hard on the gland follower. Over-tightening scorches the PTFE, glazes the contact surface, and carves grooves into the shaft. Chemical exposure charts are a decent starting point, but they ignore heat buildup, mixed solvents, and the way a chemical behaves under pressure. That is where custom PTFE blends earn their keep in real-world pumps. A graphite-filled or glass-loaded packing tuned to a specific duty cycle often outlasts a generic premium grade several times over. The manufacturers worth trusting are the ones asking about past failures, temperature swings, and how often the pump runs dry.
Contact Us
Contact Person: Tommy Xiao
Email: [email protected]
Tel/WhatsApp: 8615651509888
Website: https://www.ptfe-factory.com